Parent Company vs. Manufacturing Subsidiary Relationship
DHV Brother Spices & Agri Export (Parent Company) is the international export merchant that originates, consolidates, finances, charters, and exports all 55 commodities. DHV Brother Spices & Agri Export is our integrated manufacturing subsidiary that physically owns and operates processing facilities for selected product lines — specifically Dehydrated White Onion (5 grades), Dehydrated Garlic (5 grades), Blanched Peanuts, Hulled & Sortex Sesame Seeds, milled pulses, and pulverization suites. Unprocessed bulk commodities (e.g. Raw Cotton, Castor Seeds, Raw Rice, Rapeseed Meal) are traded directly by the parent company through certified APMC networks and crushing mills.
Precision Food Processing Machinery & Cleanroom Facilities
Located in Mahuva (the heart of India’s white onion basin) and Gondal (Gujarat’s premier groundnut corridor), our subsidiary facility operates under food safety management systems audited for ISO 22000 and HACCP compliance.
Our infrastructure is engineered for zero cross-contamination, equipped with stainless steel SS-304 contact surfaces, multi-stage hot air continuous belt dehydrators, dust cyclonic collectors, and computerized packaging units.
Subsidiary Processing Units Overview
Unit 1: Onion & Garlic Dehydration Complex
Automatic washing flumes, peeling lines, precision rotary slicers, 5-tier multi-zone dryers, and granulizers producing Flakes, Chopped, Minced, Granules, and Powder.
Unit 2: Peanut Blanching & Splitting Line
Thermal dry blanching, soft rubber de-skinning, optical split segregation, electronic metal detection, and vacuum brick packaging.
Unit 3: Buhler Optical Sortex Cleaning Hub
High-capacity air-screen separators, gravity tables, and Buhler trichromatic color sorters for Sesame Seeds, Cumin, Fennel, and Pulses.
Unit 4: Water-Jacketed Spice Pulverizing
Chilled pin and hammer mills converting Turmeric, Chili, and Coriander into fine powders without burning volatile flavor compounds.
Core Processing Lines & Equipment
Take a visual tour of our specialized machinery engineered for continuous operation, optical purity, and strict microbiological standards.
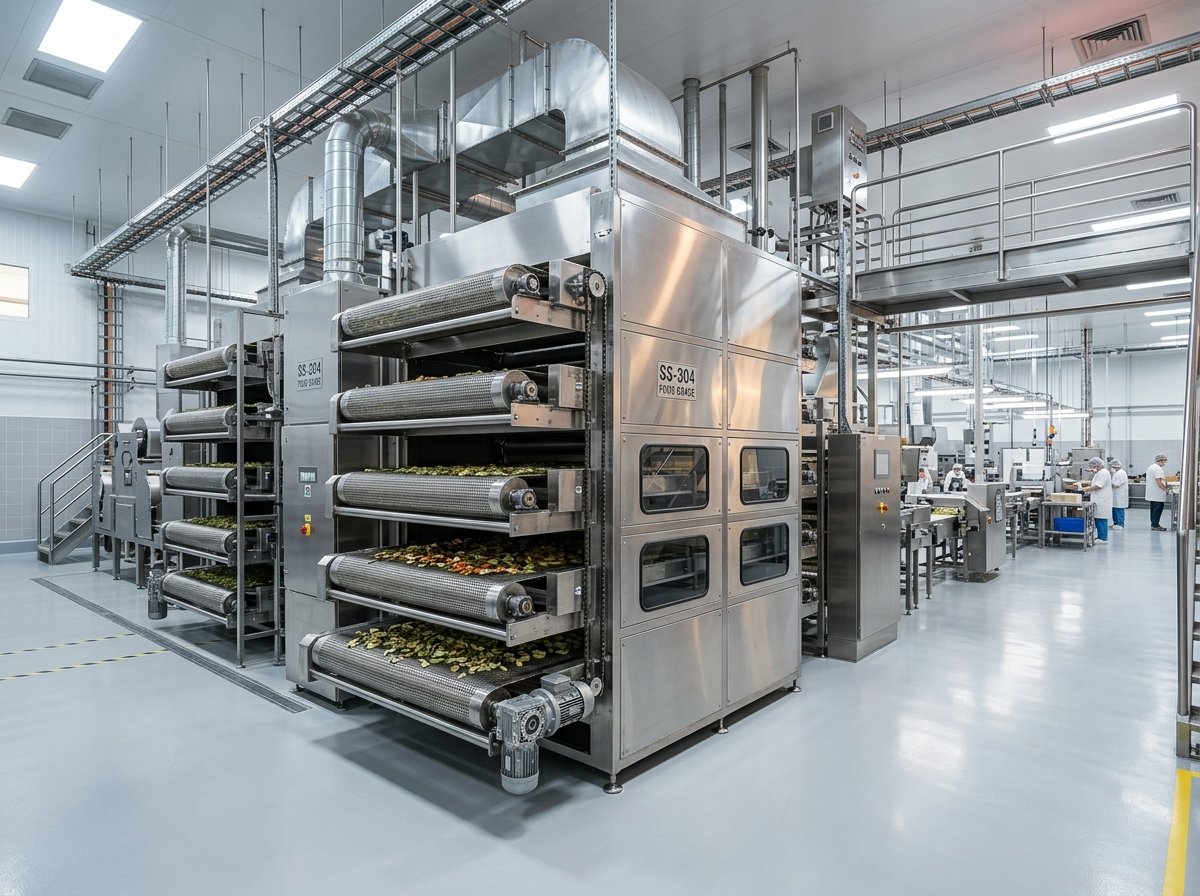 45 MT/Day Intake
5-Tier Continuous Belt Dryers
Mahuva Dehydration HubMulti-zone low temperature air circulation (45°C - 65°C) preserving allicin pungency and crisp color across kibbled flakes, granules, and powder.
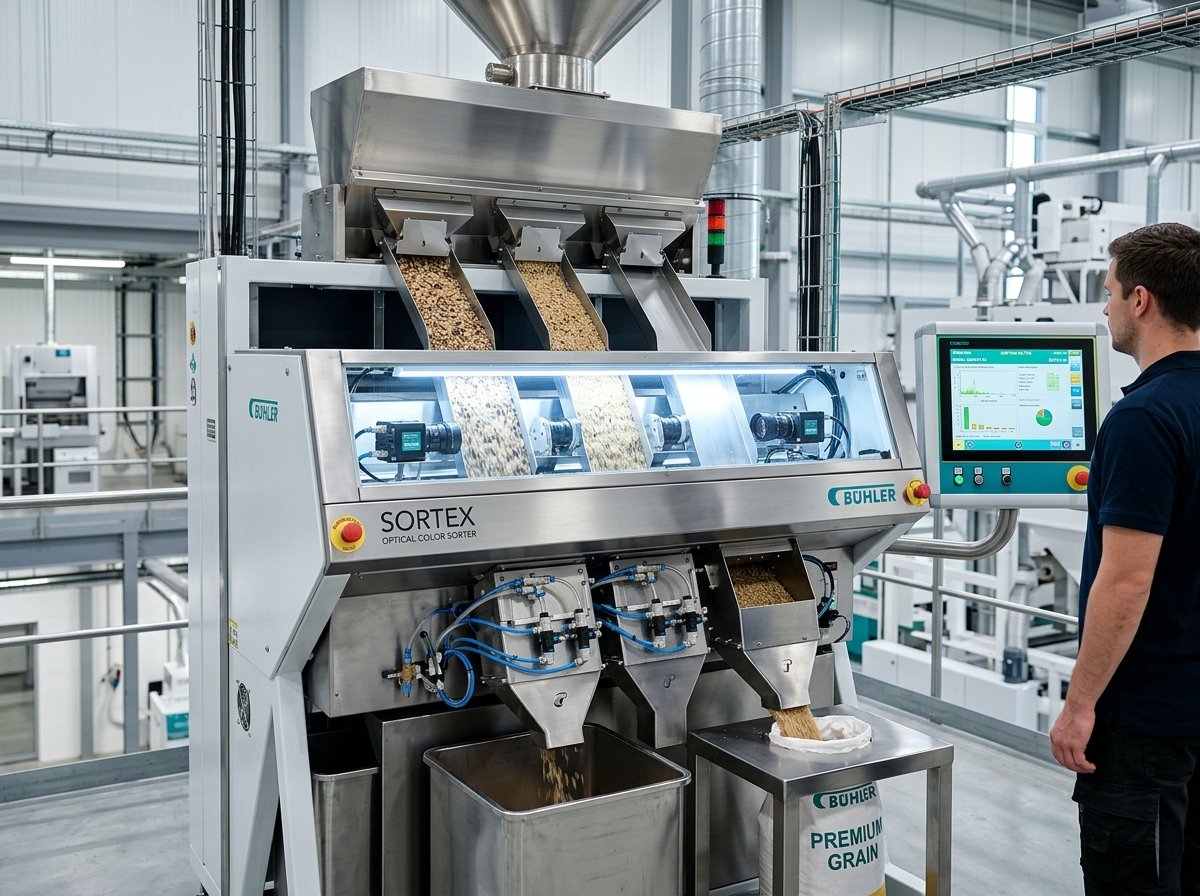 99.98% Purity
Buhler Trichromatic Sortex
Dual NIR & CCD CamerasHigh-speed optical rejection of discolored grains, foreign seeds, glass, and stones for Hulled Sesame, Cumin, and Psyllium.
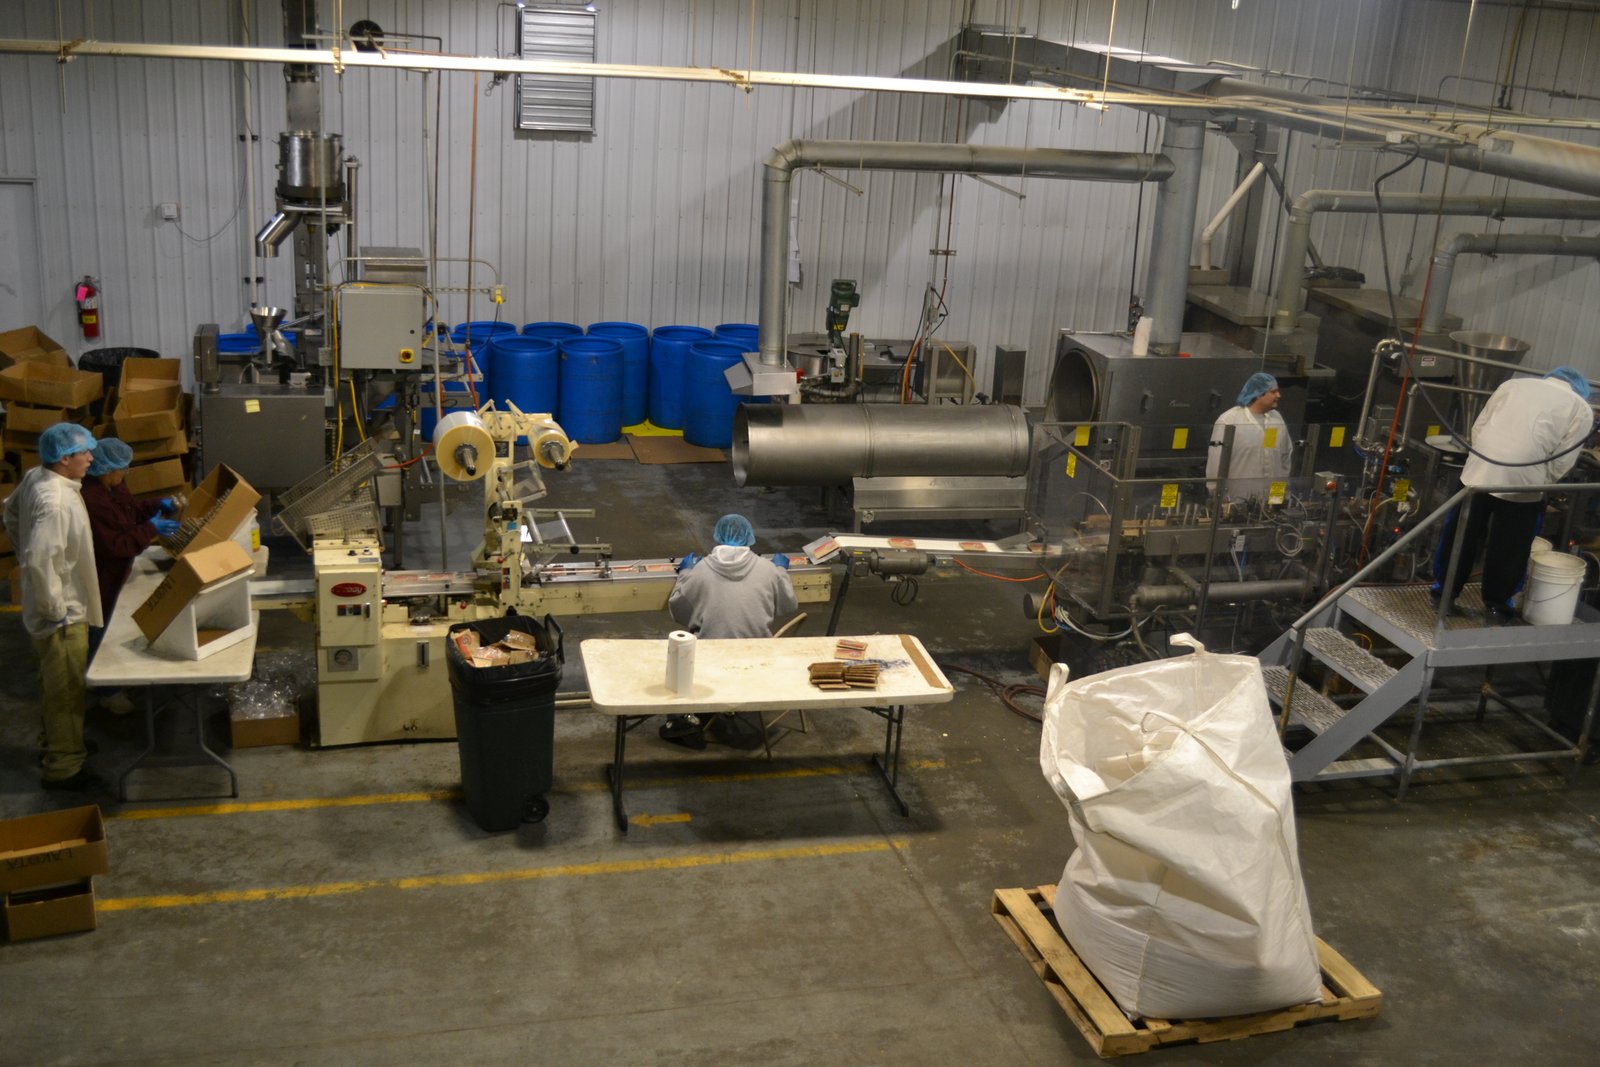 99.5% Skin Removal
Peanut Blanching Complex
Gondal Processing PlantGentle dry heat conditioning followed by soft rubber roller peeling and optical split sorting. Vacuum packed in 25kg foil cartons.
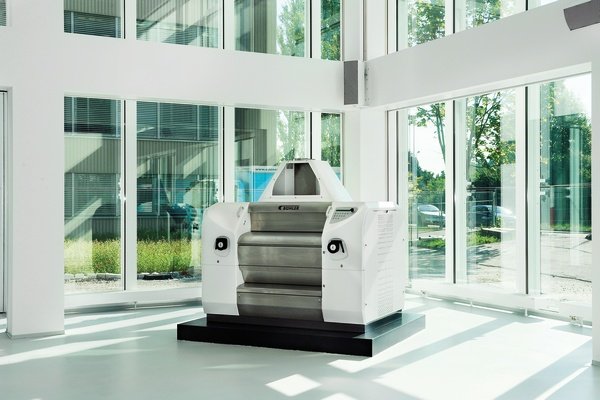 Cold Grinding
Cryogenic Spice Mill
Water-Jacketed PulverizerMaintains grinding chamber temperature below 40°C, preventing oil evaporation in Turmeric, Chili, and Coriander powders.
Installed Machinery & Output Capacity Matrix
| Processing Line | Location | Installed Technology | Rated Capacity | Target Products |
|---|---|---|---|---|
| Continuous Dehydration Suite | Mahuva, Gujarat | 5-Tier SS-304 Multi-Zone Hot Air Dryers | 45 MT / Day Fresh Intake | White Onion Flakes, Garlic Granules & Powders |
| Peanut Blanching Line | Gondal, Gujarat | Thermal Conditioning & Rubber De-Skinning | 35 MT / Day | Blanched Peanuts (Whole & Splits) |
| Optical Sortex Grading | Rajkot Hub | Buhler Trichromatic & InGaAs NIR Sorters | 5 MT / Hour | Hulled Sesame, Cumin, Fennel, Psyllium |
| Micro-Pulverization Suite | Mahuva Hub | Water-Jacketed Chilled Pin & Hammer Mills | 12 MT / Day | Turmeric Powder, Chili Powder, Garlic Powder |
| Nitrogen / Vacuum Packaging | All Units | Automated Brick Carton & Multi-Wall Poly Sealers | 60 Packs / Minute | 25kg Vacuum Bricks, Nitrogen Pouches |